
The SSAW pipes types manufactured by our tube making machine:
|
High Temperature Seamless Pipe |
ASTM A106 Gr. B/C, API 5L Gr. B, ASTM A53 Gr. B |
|
Heat Exchanger Seamless Tube |
ASTM A179 |
|
Low Temperature Seamless Pipe |
ASTM A333 Gr. 3/6 |
|
Low Temperature Seamless Tube |
ASTM A334 Gr. 6 |
|
High Yield Seamless Pipe |
API 5L Gr. X42/X46/X52/X56/X60/X65/X70/X80 PSL-1/PSL-2 |
|
High Yield Seamless Pipe |
ISO 3183 Gr.L245, L290, L320, L360, L390, L415, L450, L485 |
|
Atmospheric & Low Temp EFW Pipes |
ASTM A671 Gr. CC60/CC65/CC70 |
|
High Pressure & Moderate Temp EFW Pipes |
ASTM A672 Gr. B60/B65/B70/C55/C60/C65/C70 |
|
High Yield ERW/SAW Pipe |
API 5L Gr. X42/X46/X52/X56/X60/X65/X70/X80 PSL-1/PSL-2 |
|
High Yield ERW/SAW Pipe |
ISO 3183 Gr.L245, L290, L320, L360, L390, L415, L450, L485 |
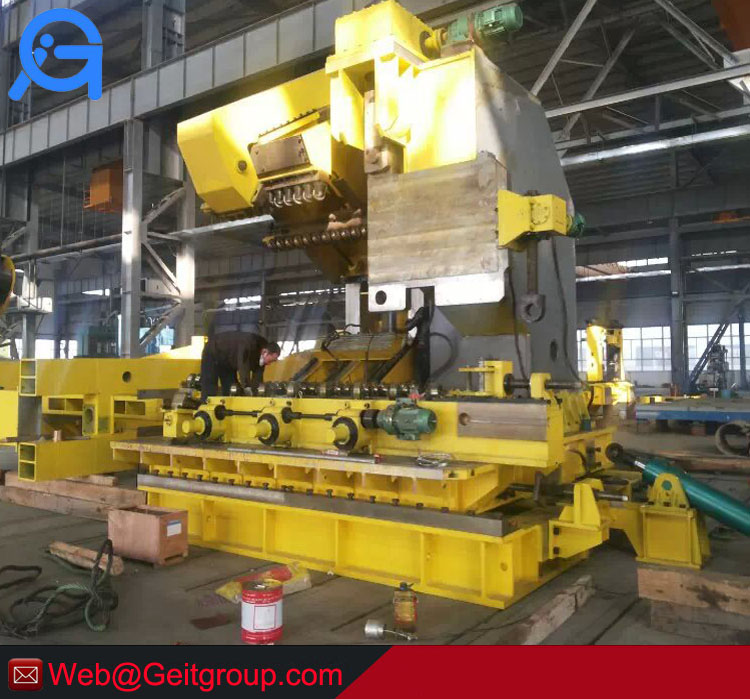
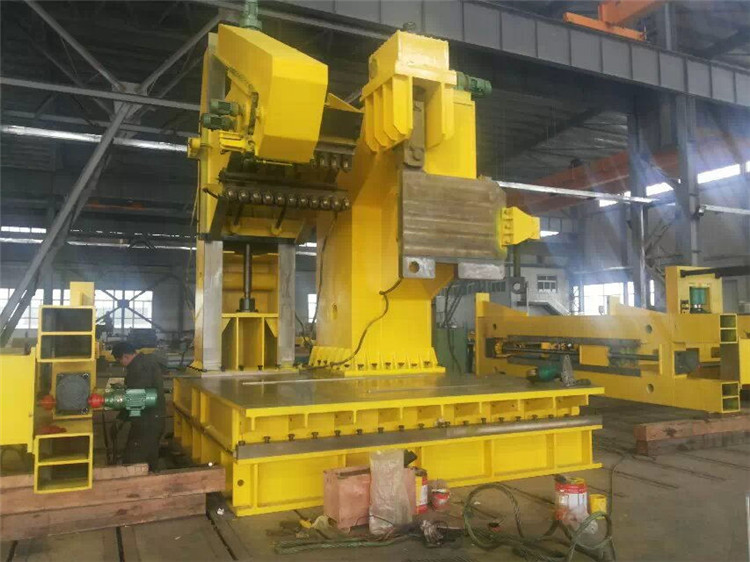
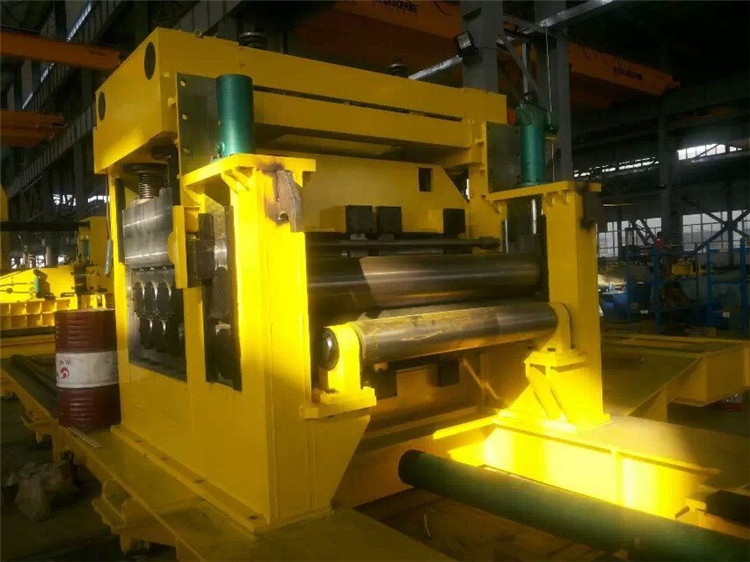
A typical SSAW pipe and tube making machiine consist of:
1. Coil Probe: steel coil into the production line, the first full board Ultrasonic Inspection
2. Leveling Milling: through anvil plate leveling machine so that the original curl, and then pass the two edges of steel-sided milling machine milling, so that up to the requirements of the plate width, plate edge parallel groove shape
3. Cut Type: steel production line along the outer edge of the coiled-coil tube
4. welding and cutting: the use of advanced technology for pre double submerged arc welding(dsaw) cutting inside from the foot of the welding specification welded steel pipe welded outside use, etc.
5. Visual inspection: some basic parameters by a professional technician check
6. ultrasonic flaw: the inner and outer sides of the base metal and weld seam 100% inspection
7. X-ray detection: internal and external welds 100% X-ray television industry checks, the use of image processing system ensures detection sensitivity
8. Pressure test: hydrostatic testingmachine by-root test steel pipe up to the standard requirements to ensure that the test pressure
9. Chamfer level: steel pipe inspection pipe end processing, up to the requirements of the pipe end beveling size
10. Check: X-rays and then subjected to ultrasonic testingand magnetic particle inspection conducted pipe end, check whether the deposit welding problems and defects in the pipe ends.
11. Oiled Marking: Qualified oiled steel pipe corrosion and in accordance with user requirements for marking.
GEIT GROUP
Tel:+86 0317-5670260
Whatsapp:+8617832978885 +8618803375788
Fax:+86 0317-5670259
Email:[email protected]
Address:Room711,Culture building, Beijing Road, Yunhe District, Cangzhou City, Hebei,China